Table of Contents
- Map the Sorting Workflow Before Writing Any Bag Spec
- Treat Material and Structure as Decision Criteria, Not a Catalog
- Specify Handles, Openings, and Label Pockets for Real Ops
- Build Color Coding and Identification for Multi-Site Fleets
- Lock Acceptance Records and Release Gates in the Procurement File
- Define OEM Customization Scope Around Fit and Identification
- Ask Supplier Questions That Protect the Purchase Decision
- Frame Total Cost of Ownership Beyond Unit Price
- Standardize Rollout Across Depots Without Over-Customizing
- Decide When Custom OEM Beats Standard Sorting-Bag SKUs
Map the Sorting Workflow Before Writing Any Bag Spec
Procurement teams that start with a fabric swatch or a product photo often discover misfit after the first delivery wave. A better sequence begins with the physical path of a parcel: where it is scanned, where it is grouped, how far a filled bag travels, and whether workers lift, slide, drag, or stage the tote on racks and cages. That map should name each station that will touch Logistic Sorting Bags, from inbound consolidation to outbound vehicle loading and empty-bag return.
Write the workflow in plain operational language. Note aisle width, shelf clearances, cage footprints, and typical parcel mix. Capture whether bags stay open during rapid chute discharge or need a closure for hub-to-hub transfer. Record peak shift volume and how many bags sit in staging at once. These facts drive finished dimensions, opening style, base construction, and identification layout more reliably than generic capacity language.
Involve warehouse supervisors and route planners before the RFQ is frozen. Procurement can still own commercial terms, but operators know which handle height slows a two-person lift and which label pocket disappears behind a cage bar. When the workflow map is complete, convert it into a short specification brief: intended stations, handling method, environment notes, and identification rules. That brief becomes the shared reference for sample requests, OEM drawings, and later replenishment. Buyers comparing Parcel Sorting Bags across vendors then evaluate against the same operational checklist instead of competing slogans.
Treat Material and Structure as Decision Criteria, Not a Catalog
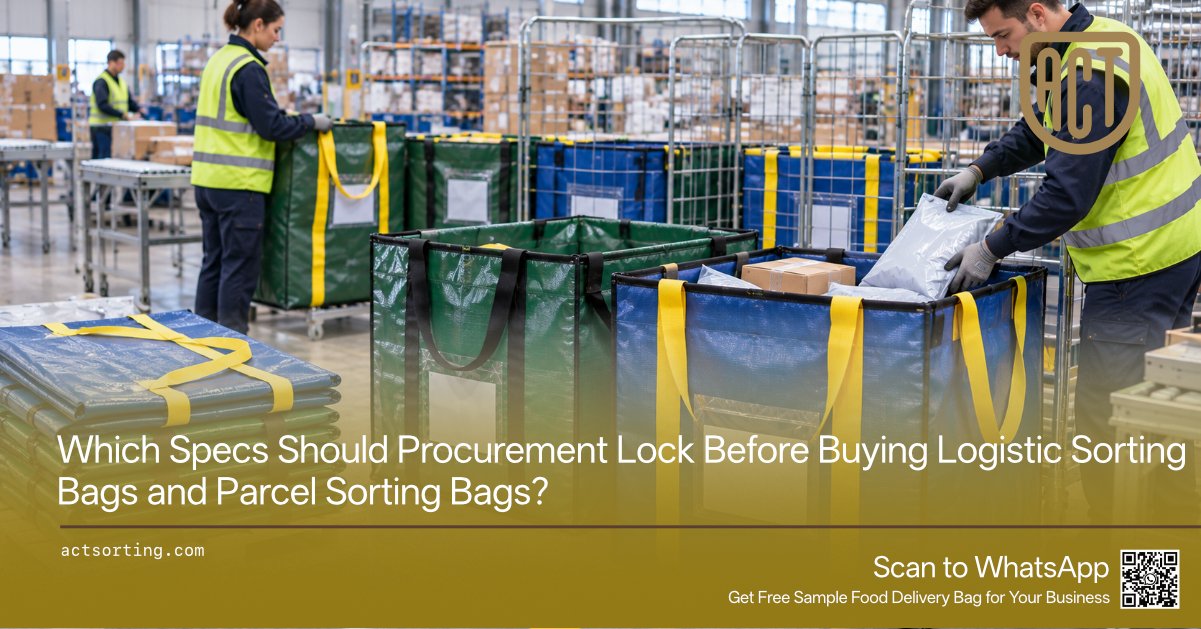
Material choice should answer how the bag will be handled, cleaned, folded, and stored—not which fabric name sounds strongest in a brochure. PP woven constructions are common for reusable warehouse sorting because they combine tear resistance, relatively low weight, and compact folding after empty return. Oxford and coated textile options may suit programs that prioritize wipe-down surfaces or a different hand feel. Foldable body geometry matters when empty bags must stack in limited depot space. A plastic runner base or rigid board insert can stabilize mixed cartons when bags are slid along floors or shelves, while a fully flexible base favors denser packing for reverse logistics.
Procurement should score structure against the workflow map. Ask whether bags will stand under a discharge point, nest inside a roll cage, or ride vehicle shelves with limited height. Rectangular, warehouse-ready profiles usually stage more predictably than soft, irregular sacks. Reinforced upper edges and industrial-grade webbing attachment zones reduce early failures at lift points. Laminated or coated faces can simplify cleaning after dusty or damp dock work, but coatings also affect fold thickness and packing density.
Avoid treating “thicker fabric” as a universal upgrade. Seam layout, handle reinforcement, and base design often determine field life more than a single material claim. Request clear descriptions of body fabric, edge binding, webbing, closure type, and optional base inserts, then match each element to a known handling stress. ACTSORTING develops reusable sorting equipment around dimensions, materials, structure, and identification details rather than one fixed SKU story; buyers can use that flexibility to shortlist configurations that fit the map instead of forcing operations onto an unrelated catalog item. Keep the scorecard factual: fitness for lift method, fold storage, moisture exposure, and visual identification—not invented durability percentages.
Specify Handles, Openings, and Label Pockets for Real Ops
Handles are high-cycle wear points. Specify webbing width, attachment length, stitching pattern expectations, and handle count relative to bag size and lift style. Side handles help pull a filled tote from vehicle shelving; longer upper grips support short carries between staging lanes. Contrasting handle colors improve grip location in crowded docks, but color alone does not equal strength—attachment design does. Ask suppliers to show how reinforcement distributes load into the body fabric rather than concentrating stress on a small sewn patch.
Opening geometry controls cycle time. Wide open-top mouths speed chute and table loading; zippers or hook-and-loop closures help contain parcels during longer transfers. Choose based on station tempo: a hub transfer bag may justify a closure that would slow a last-wave driver who opens the same tote dozens of times. Upper-edge reinforcement keeps partially filled bags workable when workers reach for mixed poly mailers and cartons.
Transparent route label pockets belong in the same specification block. Pocket size, placement, and readability from normal walking height affect mis-sort risk across multi-route staging. Confirm whether cards insert from the top or side and whether branding or barcode panels compete with the pocket for visual space. ACTSORTING lists handles, openings, closures, branding, NFC chips, unique barcodes, and transparent route label pockets among customization levers for logistics bags; procurement should treat those as selectable ops features, not optional decoration. When the RFQ names handle layout, opening method, and pocket placement in one place, sample evaluation becomes faster and fewer units arrive with “almost right” geometry that slows every shift.
Build Color Coding and Identification for Multi-Site Fleets
Multi-depot fleets rarely fail from fabric alone; they fail when bags cannot be recognized at a glance. Color coding should map to a controlled taxonomy—region, service class, return stream, or priority lane—so workers do not invent local meanings. Document the palette in the master specification: body color, webbing contrast, and any secondary markers such as edge binding. Require that replenishment orders match the approved combination so a later batch does not break the visual system.
Identification layers should stack without conflict. Permanent branding can mark ownership for reverse logistics. Unique barcodes or NFC options support asset tracking when the network needs bag-level accountability. Transparent pockets carry temporary route cards that change by wave. Write rules for what is fixed versus what is wave-level so printing and chip placement do not block the pocket. Train receiving teams to reject shipments that omit the agreed ID elements.
Standardize naming across sites. Call the same SKU the same thing in every depot’s inventory list, and attach a photo of the approved colorway and pocket layout. When new facilities open, ship a starter kit of Logistic Sorting Bags already coded to the network map rather than letting each site invent a private scheme. ACTSORTING supports custom branding, logo application, NFC chips, unique individual barcodes, and transparent route label pockets as part of sorting-bag development; procurement can embed those options into a fleet ID policy instead of treating them as one-off print requests. Clear identification reduces misloads between hubs and keeps empty-bag returns flowing to the correct owner.
Lock Acceptance Records and Release Gates in the Procurement File
A purchase decision is incomplete until the buying organization can prove what was approved, by whom, and against which physical master. Build a procurement file for Logistic Sorting Bags that travels with the SKU from first RFQ through every replenishment lot. At minimum, archive the workflow brief, the frozen dimension and identification specification, supplier quotations with open-item lists, signed sample approval forms, drawing or artwork revisions with dates, and photographs of the approved master unit from front, side, open mouth, label pocket, and base. Store digital copies in a controlled folder and keep one physical master sample tagged with the SKU code, approval date, and revision letter.
Define release gates before bulk production and again before warehouse put-away. Typical gates include: specification freeze (procurement and operations co-sign), sample acceptance (operations lead signs handling fit; procurement signs commercial match), pre-shipment inspection evidence received and reviewed, and inbound receiving clearance against the master. Name the roles in writing—network engineering or warehouse supervisor for operational fit, procurement for commercial and document completeness, quality or receiving for lot comparison—so approvals do not stall on informal chats. Record fail reasons with measurable deltas (for example, height above shelf clearance or pocket card that does not seat) rather than vague dissatisfaction.
When replenishment arrives, receiving should pull the master sample and the approved checklist, then compare critical dimensions, webbing color, pocket placement, branding, and base construction on a sample of cartons before releasing the lot to floor stock. Quarantine mismatches; do not “use them up” into a coded fleet. For field-trial methods that informed the original approval—clearances, handles, folding, and workflow fit—point teams to ACTSORTING’s PP woven sample readiness guidance as extended reading, while keeping this section focused on documentation, sign-off authority, and lot release control. A clean file lets new depot managers inherit the same Parcel Sorting Bags standard without rediscovering tribal knowledge.
Define OEM Customization Scope Around Fit and Identification
OEM work pays off when a standard SKU cannot clear a hard constraint: shelf height, cage footprint, dual-handle lift pattern, bilingual pocket size, or fleet-wide branding rules. Scope customization to the constraints that change handling outcomes. Typical levers include finished dimensions, material selection, handle count and placement, opening and closure type, reinforced zones, optional base inserts, body and webbing colors, logo branding, NFC chips, unique barcodes, and transparent route label pockets. That list matches the customization themes ACTSORTING describes for sorting-bag / logistics-equipment programs and stays within what a competent custom manufacturer can reasonably quote.
Resist decorative scope creep. Extra panels, unused pockets, or complex prints that do not serve sorting speed or identification add cost and sampling cycles. Write acceptance criteria for each custom element: maximum height for a named vehicle shelf, minimum pocket card size, required barcode placement relative to the pocket, and fold thickness targets for empty return. Approve drawings and a physical sample before bulk release. Ask how future replenishment will lock the same bill of materials so the second order does not silently change webbing or coating.
Use OEM to standardize a network, not to create a unique bag per depot. One approved custom profile shared across sites usually beats a patchwork of near-identical variants. When the constraint is soft—preference rather than clearance failure—test a standard parcel sorting bag category first. Custom development is justified when the workflow map shows repeated friction that a stock geometry cannot remove.
Ask Supplier Questions That Protect the Purchase Decision
Strong supplier questions expose process quality before money moves. Ask how requirement review, design, sampling, approval, bulk production, and inspection are sequenced. Request clarity on which details are confirmed on the quotation: dimensions, materials, handles, closures, pockets, branding, barcoding or NFC options, packing method, and which items remain open. Confirm how change requests are documented after sample approval so verbal tweaks do not become silent production drift.
Ask what the supplier needs from the buyer to avoid rework: photos of current bags, cage or shelf measurements, route-card sizes, color references, artwork files, and a description of lift and staging methods. Probe packing definitions early—pieces per individual pack versus pieces per master carton—because logistics receiving and freight planning depend on those numbers. Inquire how quality checks cover materials, dimensions, workmanship, and functional details against the approved sample, without demanding invented test certificates the buyer cannot validate.
Ask who owns communication during production and what inspection evidence ships with the goods. Request references to comparable sorting-bag programs in general terms rather than fabricated carrier partnerships. Review public product and news context on ACTSORTING and related news updates to understand positioning, then verify specifics in writing for the live project. Confirm in one line whether the next physical unit needed is a stock reference or a customized sample for the frozen specification, and keep detailed field-trial methods out of the RFQ Q&A—those belong in the acceptance file and, where useful, in ACTSORTING’s PP woven sample readiness guidance. Written answers become part of the vendor file and reduce later disputes.
Frame Total Cost of Ownership Beyond Unit Price
Unit price is visible; friction cost is not. Total cost of ownership for Parcel Sorting Bags includes sampling cycles, freight and packing density, receiving time, mis-sort risk from weak identification, early replacement from poor handle or seam design, empty-bag reverse logistics, and the labor lost when bags do not fit cages or vans. A cheaper tote that fails clearance checks can force double handling every wave. A slightly higher-spec, industrial-grade configuration that matches shelves and color codes can reduce those recurring losses without any invented savings percentage.
Build a simple TCO worksheet. List purchase price, expected packing volume impact on inbound freight, estimated handling minutes per filled move, storage space for empties, and replacement triggers observed in pilots. Compare two or three configurations on that sheet using the buyer’s labor rates and freight assumptions—not supplier marketing math. Include the cost of a second sample round if the first geometry misses, and the cost of stranded inventory if a nonstandard colorway cannot be reused elsewhere in the network.
Favor specifications that protect reuse and foldable return density when empty transport is a real expense. Reusable, warehouse-ready bags only deliver value when they stay in circulation and remain identifiable. Document assumptions so finance and operations share the same model. Avoid quoting unverified lifespan years or abrasion scores; let pilot performance set replacement intervals. When TCO is framed this way, OEM fees for the right dimensions or pockets look like risk control rather than optional decoration, and standard SKUs look appropriately cheap only when they already clear the workflow map.
Standardize Rollout Across Depots Without Over-Customizing
Rollout fails when each depot improvises. Publish a network standard: approved dimensions, materials, color codes, handle layout, pocket rules, and naming conventions for Logistic Sorting Bags. Issue a one-page visual guide with photos of the approved sample, card insertion method, and empty fold. Train supervisors before the first bulk drop so receiving knows what to accept and what to quarantine.
Phase introduction by site criticality. Start with one high-volume depot, run the sample protocol under live parcels, lock the specification, then expand. Keep a central SKU owner in procurement or network engineering so local reorders cannot quietly change color or pocket size. Maintain a small buffer of approved bags for surge weeks rather than authorizing emergency buys of unrelated shapes that pollute the fleet.
Balance standardization with limited controlled variants. A network may need two heights for different vehicle classes, but those variants should be named, photographed, and barred from casual substitution. Retire legacy bags on a schedule so mixed generations do not confuse route coding. Share lessons through internal ops notes and keep the buyer’s master specification as the only acceptance authority across sites. Standardization is a procurement control system: same inputs, same acceptance checks, predictable replenishment.
Decide When Custom OEM Beats Standard Sorting-Bag SKUs
Choose standard SKUs when clearances, lift patterns, and identification needs already match an available model, when the program is a pilot, or when speed to first shipment matters more than perfect branding. Choose custom OEM when a hard constraint repeats across sites: shelf height conflict, cage misfit, missing dual-side handles, insufficient pocket size, mandatory barcode or NFC placement, or a locked corporate color system that stock options cannot meet. Put the stock-versus-OEM call in a single procurement note after one live trial: stay standard if the shift runs clean; open a limited OEM scope only for the constraints that forced workarounds, then approve one network master profile rather than a drawing per depot.
Revisit that note at replenishment if vehicles or cages genuinely change. For buyers ready to move from checklist to quotation, share the workflow map, target dimensions, color codes, handle and pocket requirements, estimated volume bands, and photos of current pain points with ACTSORTING. Request a structure recommendation aligned to those inputs, then lock acceptance criteria and sign-off roles before bulk production. That sequence keeps Logistic Sorting Bags and Parcel Sorting Bags purchases tied to operations instead of catalog impulse—and gives procurement a clean audit trail from need to approved equipment.
FAQ
Q1: What information should procurement send before asking for a logistic sorting bag quotation?
A1: Send the workflow map, finished dimension targets or clearance limits, handling method (lift, slide, stage), preferred materials, color-coding rules, handle and opening preferences, label-pocket or barcode/NFC needs, estimated quantity bands, and photos or drawings of current bags or cages. Clear inputs reduce sample rework.
Q2: How should buyers compare PP woven and Oxford options for parcel sorting bags?
A2: Compare them against fold storage, cleaning needs, moisture exposure, and how bags move in the facility. PP woven is widely used for reusable warehouse sorting; Oxford or coated textiles may suit programs that prioritize wipe-down surfaces. Score fitness to the workflow rather than fabric marketing names.
Q3: When is a stock-color sample acceptable during OEM evaluation?
A3: A stock-color sample is often enough when the priority is checking dimensions, handles, closures, base behavior, and vehicle or cage fit. Request a color-matched sample when route coding or brand approval depends on the exact palette before bulk release.
Q4: Which identification features belong in a multi-depot sorting-bag standard?
A4: Define body and webbing colors, ownership branding, transparent route label pocket rules, and whether unique barcodes or NFC chips are required for asset control. Separate fixed identity elements from wave-level route cards so printing does not block daily labeling.
Q5: What signals that a network should move from standard SKUs to custom OEM?
A5: Repeated clearance failures, handle layouts that force awkward lifts, pockets too small for route cards, or a mandatory fleet color and barcode scheme that stock models cannot meet. If a live sample trial needs constant workarounds, limit OEM scope to those constraints and approve one network master profile.